The Composition of Crude Corn Oil Recovered after
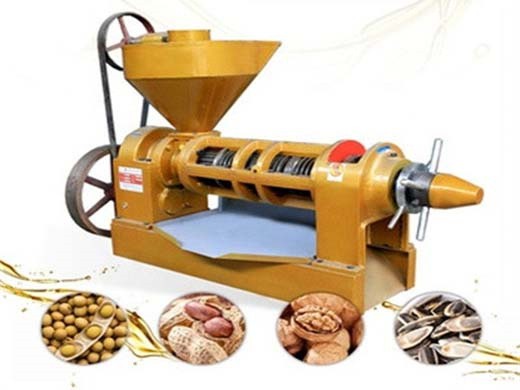
- Usage:Corn germ Oil
- Type:Cold & Hot Pressing Machine
- Automatic Grade:Automatic
- Production Capacity:1~1000T/D
- Voltage:Up to specification
- Power(W):Up to specification
- Dimension(L*W*H):Up to specification
- Weight:Up to specification
- Certification:ISO,SGS,BV
- After-sales Service Provided:Engineers available to service machinery overseas
- Material:Carbon steel
A study was conducted to examine the chemical composition of corn oil obtained after fermentation of corn to make fuel ethanol via centrifugation and compare its composition to that of corn germ
Corn oil was extracted using an aqueous enzymatic oil extraction process made from wet milled corn germ milling the germ, incubating it with cellulase enzyme, and centrifugation to separate the free oil were all part of the process.
Aqueous Extraction of Corn Oil After Fermentation in the Dry
The chemical composition and appearance of the various corn oils can be very different based on the feedstock (corn germ, ground corn, corn fiber, etc.) and extraction process (pressing, hexane extraction, aqueous enzymatic extraction, post-fermentation centrifugation, etc.) used to produce the oil.
An improved aqueous extraction method has been established for extraction of oil from corn germs. This method primarily included steam explosion pretreatment and aqueous ethanol extraction. Process variables such as steam pressure, resident time,
AQUEOUS ENZYMATIC EXTRACTION OF CORN OIL AND VALUE-ADDED
Goals / Objectives Develop new environmentally safe aqueous/enzymatic processes to extract the edible oil from corn germ (obtained from new-generation dry-grind corn-to-ethanol plants) and develop processes to fractionate the de-oiled germ into value-added protein and carbohydrate coproducts, to improve the overall economics of making fuel ethanol in new-generation plants.
The corn germ oil extracted by the aqueous enzymatic method had better quality indexes in comparison with that exacted by the solvent. The fatty acid compositions of corn germ that was oil-extracted by two kinds of methods had almost no significant differences.
The first stage of refining of post-fermentation corn oil
Post-fermentation crude corn oil obtained as a by-product in the production of bioethanol from maize grains is characterized by a very high content of free fatty acids. Refining of post-fermentation corn oil will give a product that will be different from the refined oil obtained by extracting oil from corn germs.
Aqueous enzymatic extraction of corn germ oil was investigated. By applying hydrothermal pretreatment of corn germ, it was possible to inactivate native enzymes present in the germ and to loosen its structure. The corn was then ground and treated with enzymes. After the oil had been released by the enzyme reaction, it was separated by
Aqueous Extraction of Corn Oil After Fermentation in the Dry
Conclusions Corn ethanol production, quality of coproducts, germ separation, and oil recovery have been enhanced with component recovery either before or after fermentation.
This work extends aqueous extraction to dry-mill germ, a fraction containing 15-20% oil that can be separated from corn at dry grind plants for a low retrofitting cost. Technical Abstract: The many recent dry grind plants that convert corn to ethanol are potential sources of substantial amounts of corn oil.